
Mechanical Seals in the Pharmaceutical Industry: Precision, Safety, and Regulatory Compliance
In the pharmaceutical industry, every detail counts, from product quality to process precision. Mechanical seals are essential components for ensuring safety and efficiency in critical equipment such as mixing, homogenization, and liquid processing systems. They also comply with strict Good Manufacturing Practice (GMP) regulations, offering the reliability this highly regulated sector requires.
Innovation and Safety in Every Seal
Optimize Your Operations
Discover how our mechanical seals can transform the efficiency of your industrial processes.
PRODUCTS

Seal Codes
Seal codes simplify the selection of industrial products by providing detailed specifications that ensure compatibility and performance.

Cartridge Seals
The cartridge seal is an advanced mechanical seal solution that simplifies installation and maintenance in industrial equipment, ensuring efficiency and safety.

Cooling and Reservoir
Cooling and reservoir systems play a fundamental role in the efficiency and safety of mechanical seals used in various industrial applications. These systems ensure seals operate under optimal conditions.

Metal Bellows Seals
Metal bellows seals are key industry components, designed to provide effective sealing under demanding conditions. Their robust structure and high-quality materials allow them to operate across a wide range of temperatures and pressures.

Standard Seal
The standard seal is a critical component in the sealing industry, designed to prevent fluid leaks and ensure the integrity of mechanical systems. Its robust construction and high-quality materials guarantee reliable performance and a long service life,

Dry-Running Seal
The dry-running seal is an innovative component that operates without the need for lubrication, making it ideal for applications where fluid contamination is a risk.

Mixer Seal
Mixer seals are crucial components in various industrial applications, especially in processes involving the mixing of liquids and solids. These seals are designed to prevent material leaks.

Sink Roll Seal
The sink roll seal is an essential component in plumbing systems, designed to prevent water leaks and ensure a tight seal. Made with high-quality materials, this seal offers durability and corrosion resistance.

Special Tasks
Special tasks are activities that require specific skills and a detailed approach for proper execution, especially in industrial environments. These tasks are essential to ensuring the quality and efficiency of processes.
Mechanical Seals in the Pharmaceutical Industry
In the pharmaceutical industry, mechanical seals are critical components designed to ensure the integrity, purity, and safety of production processes. These seals provide a tight seal on key equipment, such as mixing, homogenization, and liquid processing systems, preventing leaks that could contaminate sensitive products. Made with certified materials, such as stainless steel, silicon carbide, and FDA-approved elastomers, they comply with GMP (Good Manufacturing Practice) regulations and support cleaning and sterilization processes such as CIP (Cleaning in Place) and SIP (Sterilization in Place). Thanks to their resistance to chemicals, high temperatures, and pressures, mechanical seals ensure efficient, contamination-free operations, essential elements in an industry where quality and regulatory compliance are non-negotiable.
Benefits of High-Quality Mechanical Seals
- Contamination prevention: Ensure a tight, leak-free environment, preventing cross-contamination and ensuring final product purity. Durability and resistance: Designed to withstand demanding processes with chemicals, high pressures, and temperatures without compromising performance. Operational efficiency: Reduce downtime and frequent maintenance, optimizing continuous production. Regulatory compliance: Meet strict industry standards, making audits and regulatory certifications easier. Cost reduction: Extend equipment service life, minimize product loss, and reduce maintenance spending.
01
Contamination prevention
02
Durability and resistance
03
Operational efficiency
04
Regulatory compliance
05
Cost reduction


Discover More About Our Mechanical Seals
Are you ready to improve the efficiency of your operations with our high-quality mechanical seals? Contact us today to get more information on how we can help you optimize your industrial processes. Our team is here to advise you every step of the way.
Practical Application: How Our Seals Transform the Pharmaceutical Industry
Our mechanical seals are designed to adapt to the specific needs of the pharmaceutical industry, providing solutions that improve performance and ensure safety at every stage of the process. From mixing systems to liquid processing equipment, our seals offer:
- Extreme reliability: Uninterrupted continuous operations, reducing costs from unexpected failures. Custom adaptation: Specific designs for each type of equipment and fluid, optimizing performance and ensuring compatibility. Guaranteed hygiene: Materials approved for sanitary applications, with smooth surfaces that make cleaning and sterilization easier.

With our solutions, you not only meet GMP and FDA standards, but also raise the efficiency and quality of your pharmaceutical production.
Compliance with GMP Regulations and International Standards
The pharmaceutical industry is governed by strict regulations, such as Good Manufacturing Practices (GMP), which require high standards of safety and quality. Mechanical seals designed for this sector meet requirements such as:
- Compatibility with pharmaceutical products: Made with non-toxic, corrosion-resistant materials. Easy-clean installation: Designed to be easily disassembled and compatible with CIP (Cleaning in Place) and SIP (Sterilization in Place) cleaning systems. International certifications: Comply with regulations such as ISO 9001, FDA, and USP, ensuring product purity.

Different Industries
Oil and Gas Industry
- Applications: Pumps and mixers in processing systems.
- Importance: Designed to resist abrasion and handle fluids with suspended solids, ensuring operational continuity.
Power Generation Industry
- Applications: Turbines, cooling pumps, boilers, and generators.
- Reason: High temperatures and pressures in thermal and nuclear power plants.
Chemical and Petrochemical Industry
- Applications: Reactors, mixers, and chemical pumps.
- Importance: Corrosion-resistant and designed to handle aggressive chemicals, ensuring product purity and environmental safety.

Food and Beverage Industry
- Applications: Reactors, homogenizers, and process pumps.
- Importance: They comply with GMP regulations, ensuring product purity and facilitating cleaning.
Mining and Minerals Industry
- Applications: Slurry pumps and processing equipment.
- Importance: They withstand abrasive fluids and extreme conditions, reducing equipment wear and extending its service life.
Pulp and Paper Industry
- Applications: Pumps, compressors, and processing equipment.
- Importance: It withstands high pressures and extreme temperatures, preventing hazardous fluid leaks and ensuring safety and sustainability.
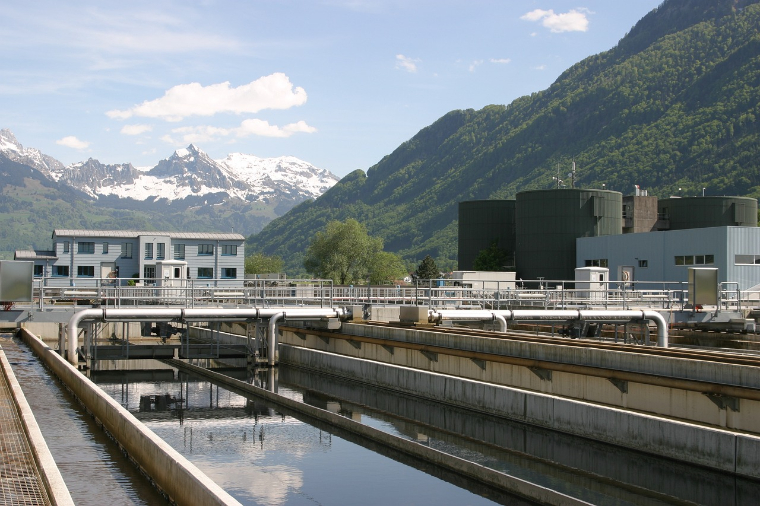
Wastewater and Clean Water Management
- Applications: Pumping systems, clarifiers, and desalination plants.
- Importance: They prevent leaks, resist aggressive chemicals, and ensure the efficiency of purification processes.

Pharmaceutical Industry
- Applications: Reactors, homogenizers, and process pumps.
- Importance: They comply with GMP regulations, ensuring product purity and facilitating cleaning.

Refrigeration Industry
- Applications: Compressors, refrigerant pumps, and cooling systems.
- Importance: They seal modern, eco-friendly refrigerants, ensuring energy efficiency and sustainability.
Polymer Industry
- Applications: Transfer pumps, extruders, reactors, and mixers.
- Reason: To withstand high temperatures, pressures, and viscous or abrasive fluids.
Optimize Your Pharmaceutical Processes with Trusted Seals
At YAR Asociados, C.A., we understand the unique demands and challenges facing the pharmaceutical industry. Our mechanical seals ensure operational efficiency, compliance with international regulations, and total protection for your processes at every production stage. Why trust us for your mechanical seals? Tailored solutions: We adapt to your specific needs with custom designs. Premium quality materials: We use FDA- and GMP-certified components, resistant to chemicals and aggressive processes. Reduced operating costs: Durable seals that minimize maintenance and downtime. Comprehensive technical support: We guide you through selection, installation, and maintenance to ensure optimal performance. Contact us today and discover how our mechanical seals can transform your pharmaceutical plant, optimizing every process so your production is safe, efficient, and uninterrupted. Trust experts who care about every detail! 🚀
Preguntas Frecuentes
1. Why are mechanical seals important in the pharmaceutical industry?
Mechanical seals ensure the containment of liquid products and prevent leaks or contamination, ensuring product purity and compliance with quality regulations.
[
2. What regulations do mechanical seals meet for pharmaceutical use?
Our seals comply with GMP, FDA, ISO 9001, and USP regulations, ensuring their suitability for pharmaceutical processes.
[
3. What materials are used in mechanical seals for this industry?
Materials used include stainless steel, silicon carbide, certified elastomers, and non-toxic components approved by the FDA.
[
4. Are they compatible with CIP and SIP cleaning processes?
Yes, our seals are designed to withstand clean-in-place and sterilize-in-place (CIP/SIP) systems without losing performance or durability.
[
5. How long do mechanical seals last in pharmaceutical environments?
With proper maintenance, high-quality seals can last for years, depending on operating conditions and the fluid being processed.
[
6. What happens if a seal fails in a pharmaceutical process?
A failure can compromise product purity and halt production. That is why we recommend high-quality seals and periodic inspections.
[
7. Can I customize a mechanical seal for my specific equipment?
Yes, we offer customized solutions tailored to the needs and specifications of your equipment and processes.
[
8. What type of maintenance do mechanical seals require?
Periodic inspection, proper cleaning, and replacement of worn components are recommended. We provide technical guidance for optimal maintenance.
[
9. How do mechanical seals contribute to operational efficiency?
They minimize downtime, reduce product losses, and optimize equipment performance, improving overall productivity.
[
10. What advantages do your mechanical seals offer over others on the market?
Our seals combine advanced materials, regulatory compliance, extreme durability, and comprehensive technical support, ensuring superior results.
[
What Our Customers Say
★★★★★
“Since we started using mechanical seals from sellosmecanicosyar.com, we’ve seen a significant improvement in our operations’ efficiency. The quality and durability are exceptional.”

Juan Pérez
Operations Manager, PetroGas S.A.
★★★★★
“The customer service and technical support we received were unmatched. The mechanical seals have exceeded our expectations in terms of performance.”

María López
Maintenance Director, Energía y Soluciones
★★★★★
“I highly recommend sellosmecanicosyar.com. Their products have been essential in optimizing our processes and reducing downtime.”

Carlos Ramírez
Chief Engineer, Refinadora del Norte